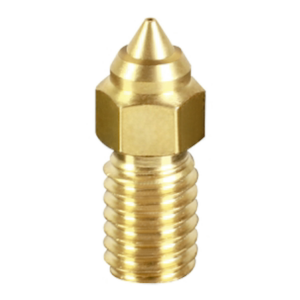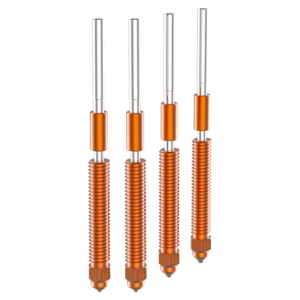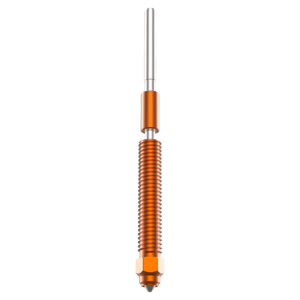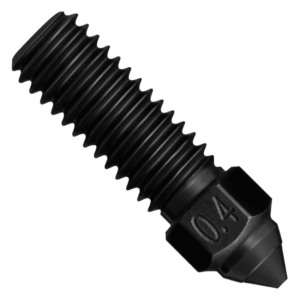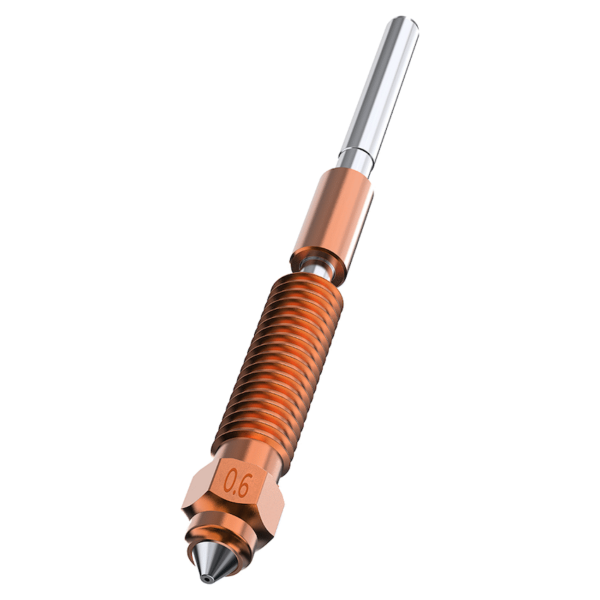

Going from 0.4mm to 0.6mm is the single cheapest way to cut hours off a large print. The wider bore and enlarged melt zone let the hotend push considerably more material per second, so thicker walls and chunkier layers stop being a bottleneck. You give up a little fine detail, which rarely matters on a bracket, a jig or an enclosure. Machined from copper alloy with a heat-resistant coating, it holds temperature steadily under the sustained flow that high-speed printing demands.
Good for
- Large functional parts and enclosures
- Structural brackets and jigs
- Cutting print time on bulky models
- Draft prints before a detailed run